-
Abrasive
-
Adhesive
-
Chemicals
-
Hand Tools
-
Hardware
-
Measurement Tools
-
Metal Markers
-
Non Sparking Tools
- Safety
-
Scaffolding Tools
-
Tooling & Cutting
- Welding
-
Welding
Welding Solutions
Professional Welding Equipment & Consumables For Every Application
Request a Quote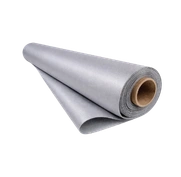
-
Safety
-
Abrasives
-
Tooling & Cutting
-
Hand Tools
-
Measurement Tools
-
Non Sparking Tools
-
Hardware
-
Chemicals
-
Metal Markers
-
Scaffolding Tools
-
Adhesive
-
Abrasive
-
Adhesive
-
Chemicals
-
Hand Tools
-
Hardware
-
Measurement Tools
-
Metal Markers
-
Non Sparking Tools
- Safety
-
Scaffolding Tools
-
Tooling & Cutting
- Welding
-
Welding
Welding Solutions
Professional Welding Equipment & Consumables For Every Application
Request a Quote -
Safety
-
Abrasives
-
Tooling & Cutting
-
Hand Tools
-
Measurement Tools
-
Non Sparking Tools
-
Hardware
-
Chemicals
-
Metal Markers
-
Scaffolding Tools
-
Adhesive
FIBACK® FIBERGLASS WELD BACKING TAPE

FIBACK® FIBERGLASS WELD BACKING TAPE
How Fiback Works
Align
Align desired base metals with the required root gap. Center the fiberglass strip over the backside of the root gap.
Position
Position the fiberglass strip in a convex shape away from the backside of the weld area to contain the purge gas from the torch tip but avoid consuming the material.
Press
Press the adhesive sections of tape along the sides of the root gap to the base metal, continuing to center the fiberglass strip. Remember to peel the release liner from the aluminum tape while progressing along the weld joint. This procedure ensures the adhesive on the aluminum tape is free from debris and foreign matter.
After Fiback has been applied to the entire length of the metals being joined, press outer adhesive edges again to create an air tight seal between the tape and the base metal.
Weld
Begin welding the desired seam.
Types & Sizes
Fiback Fiberglass Weld Backing Tape
| Item No | Description | Width | Fiberglass Center Strip Width | Length |
|---|---|---|---|---|
| AFBT-2.5-200 | Fiback Weld Backing Tape 200 AMP | 2.5″ (64 mm) | 1.125″ (28.5 mm) | 82′ (25 m) |
| AFBT-4.0-200 | Fiback Weld Backing Tape 200 AMP | 4.0″ (102 mm) | 1.5″ (38 mm) | 82′ (25 m) |
| AFBT-2.5 | Fiback Weld Backing Tape 600 AMP | 2.5″ (64 mm) | 1.125″ (28.5 mm) | 41′ (12.5 m) |
| AFBT-4.0 | Fiback Weld Backing Tape 600 AMP | 4.0″ (102 mm) | 1.5″ (38 mm) | 41′ (12.5 m) |
Heat Resistance
| Adhesive | 500°F | 260°C |
|---|---|---|
| Aluminum Foil | 1100°F | 593°C |
| Fiberglass Strip | 1022°F | 550°C |
No specification available.
| All Product / SKU | Variant | Product Code | Part Number | Unit | Status | Datasheet | View Detail |
|---|---|---|---|---|---|---|---|
| FIBACK® FIBERGLASS WELD BACKING TAPE | TRAD-327 | FIBKTPE | EA | IN STOCK | View |